If you’ve ever stood in a production room watching your chenille yarn machine suddenly go silent mid-run, you know how that sinking feeling hits—orders backed up, deadlines looming, and no clue where to start. As a chenille yarn machine supplier, I’ve worked with hundreds of mill owners, small batch producers, and even startup crafters who’ve faced this exact issue, and I’ve learned that troubleshooting these machines isn’t just about fixing parts. It’s about walking through a logical, step-by-step process that starts with the most obvious (and easiest to fix) problems before moving to more complex ones. Today, I’m breaking down how to diagnose and fix the most common causes of a stopped chenille yarn machine, drawing on years of hands-on service calls, customer feedback, and the technical specs we build into every machine we sell. Chenille Yarn Machine
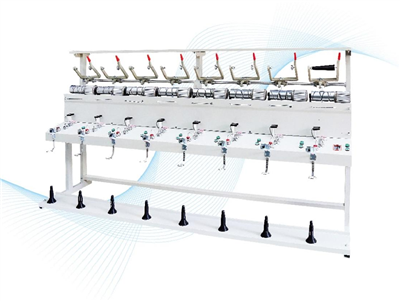
First, let’s set a quick context: chenille yarn machines are designed to loop cut pile fibers between two core yarns, creating that soft, fuzzy texture chenille is known for. They have moving parts—needle bars, feed rollers, tensioners, and gear systems—that endure constant friction, especially if you’re processing thick, high-count chenille or synthetic fibers. Over time, wear, minor misalignments, or even small material jams can throw the entire machine off, but the key is to work systematically, not panic. I always tell our customers: 80% of machine stops fall into three categories: material jams, power supply issues, or tension misalignments. Let’s start with the first, because 9 times out of 10, that’s where the problem lives.
Step 1: Rule Out Surface-Level Jams (The Most Common Culprit)
I once got a call from a customer in North Carolina who’d had their chenille machine down for two days, convinced it was a broken motor. When I arrived, I knelt down and pulled back the bottom guard of the machine, and there was a 2-inch clump of cotton chenille wrapped around the lower feed roller—small enough that a quick glance from the control panel wouldn’t catch it. Jams happen because chenille fibers are soft and prone to catching on small gaps, or if you’re using fiber that has loose ends from poor prep. Before you start taking apart major components, do a full visual inspection, and don’t just look at the parts visible through the front panel.
Start by turning off the machine and unplugging it (safety first—this is non-negotiable. I’ve seen too many small injuries from people reaching into moving parts mid-jam). Once it’s fully powered down, remove all the side and bottom guards. Chenille machines have three high-risk areas for jams: the feed roller gap, the needle bar slot, and the tensioning discs. Run your fingers gently along the length of the feed roller—if you feel any fuzzy buildup or clumps, that’s the jam. Use a soft plastic tool (not a metal screwdriver, which can scratch the roller’s surface) to loosen the clump and pull it out. Next, check the needle bar: the cut pile fibers feed through narrow slots between the needles, so if a stray fiber gets wedged there, it can stop the entire bar from moving. Again, use a soft pick to work the fiber out—never force it, because bending a needle will lead to way more problems later. Finally, check the tensioning discs, which sit on top of the machine to hold the core yarns. Loose chenille can catch between these discs, so pull them apart gently and clear any buildup.
Another thing we tell all our customers: always check the fiber preparation before you load it into the machine. If you’re using hand-processed fiber, make sure there are no loose ends or tangled clumps. For bulk orders, look for fiber that’s been carded and combed properly—frayed or low-quality fiber is the number one cause of preventable jams. I had another customer who switched to a cheaper, uncarded synthetic fiber to cut costs, and within a month, they were dealing with three jams a week. Once they went back to pre-processed, high-quality fiber, their jam rate dropped by 90%.
Step 2: Check the Power and Control System (The Obvious, But Overlooked)
If you’ve cleared all the jams and the machine still won’t turn on or run, the next stop is the power and control panel. This is another area where I see customers jump to big, expensive repairs first, when the fix is often simple. Let’s start basic: is the machine plugged in? It sounds silly, but I’ve had three customers this year who had their machine tucked in a back corner and accidentally kicked the power cord out of the outlet. Next, check the circuit breaker for the machine—most industrial machines have a dedicated breaker in the main production room, and if it tripped from a minor overload (say, from a recent big batch of thick chenille), flipping it back on will fix the issue. Don’t reset it immediately if it trips again—if it keeps tripping, that’s a sign of a bigger problem, like a faulty motor or shorted wiring, and you’ll want to have a service technician look at it.
If the machine is plugged in and the breaker is on, look at the control panel display. Most modern chenille machines (including all the models we supply) have error codes that pop up when a component fails. Common error codes we see are “low voltage,” “motor overload,” or “needle position error.” “Low voltage” is often caused by the machine being run on an extension cord that’s too thin—industrial chenille machines draw a consistent amount of power, and a lightweight extension cord can cause voltage drops that trigger the safety shutoff. If you’re using an extension cord, make sure it’s 12-gauge or thicker, and no longer than 50 feet. “Motor overload” is usually a sign that the motor is working harder than it should, often because of a hidden jam we missed, or because the machine is set to run at a higher speed than the fibers can handle. If you clear the jam and reset the motor, it should work—if not, it might be time to check the motor’s belt.
The control panel’s internal wiring can also be a culprit, especially if you’re in a dusty production environment. Dirt and lint can build up on the circuit boards over time, causing connections to slip. Once a quarter, we recommend blowing out the control panel with compressed air (on low pressure, so you don’t damage the delicate circuits) to remove any dust buildup. That small step alone has fixed more control panel issues for our customers than any other adjustment.
Step 3: Diagnose Tension and Alignment Issues (The Hidden Culprits)
If the machine runs for a few minutes after clearing a jam but then stops abruptly, or produces uneven yarn before dying, the problem is almost certainly tension misalignment or a part that’s out of sync. Chenille yarn relies on consistent tension between the core yarns and the cut pile fibers—too much tension, and the pile will pull too tight and break; too little, and the pile will bunch up, leading to friction and eventually a stall. Here’s how to check and adjust tension without calling a tech.
First, test the tension of the core yarns by pulling one of the core yarns from the feed spool. It should move smoothly, with a slight, consistent resistance—if it’s too loose, it will slip through the tensioners; if it’s too tight, it will snap when you pull. Most machines have small tension knobs on the side of the tension discs: turn the knob clockwise to increase tension, counterclockwise to decrease it. Adjust the tension for both core yarns equally—if one core has different tension than the other, the machine will pull unevenly, causing strain on the needle bar and stopping.
Next, check the alignment of the needle bar and the guide rollers. Over time, from repeated use and minor impacts, these parts can shift out of alignment. A quick way to test this is to run the machine at slow speed (most machines have a test mode) and watch the path of the cut pile fibers. If the fibers are straying from the channel between the needles, or if the needle bar is tilting to one side, that’s a sign of misalignment. Adjustment is simple: on most chenille machines, the needle bar has small set screws on the mounting bracket. Loosen the screws gently, tap the bar back into the correct position (you can use a level to make sure it’s straight), and tighten the screws. For guide rollers, look for adjustment bolts on the roller mounts—turn them slightly to align the roller with the feed roller, so fibers move straight through without catching.
I want to note here that if you’re working with a machine that’s older than 5 years, or if you’re processing a new type of fiber (like a super-thick merino wool or a stretchy spandex blend), alignment adjustments will be more frequent than with standard cotton chenille. We always include a free alignment guide with every machine we sell, and we offer a 30-minute virtual tutorial for new customers, because getting alignment right is the key to consistent, long runs.
When to Call for Professional Help (And When to Try It Yourself)
Let’s be clear: not every machine stop is a DIY fix. We always encourage customers to try the first three steps I’ve outlined, because 85% of the time, that’s all you need. But there are signs that it’s time to call a specialized technician, rather than trying to take apart a more complex component. If you hear a loud grinding or scraping noise when you turn the machine on (that’s not the normal soft hum of moving parts), that’s a sign of a broken gear or bent needle—trying to fix that yourself can lead to more damage, including cracking the machine’s frame. If the control panel isn’t displaying any error codes at all, even after checking all power sources, that’s likely a faulty circuit board, which requires specialized testing. And if your machine is still under warranty, attempting to take apart the motor or gear system will void the warranty, so it’s best to reach out to your supplier directly.
I also want to add a quick preventive maintenance tip, because the best troubleshooting is avoiding stops in the first place. We recommend scheduling a 15-minute check-in for your chenille machine every week: clear any small fibers from the guards, test the tension of a test run of yarn, and check that all set screws are tight. Every three months, do a deep clean of the feed rollers and needle bar, and check the motor belt for wear (if it’s cracked or stretched, replace it before it breaks mid-run). Our customers who stick to this schedule report 50% fewer unplanned stops than those who only work on their machine when it breaks.

At the end of the day, a stopped chenille yarn machine isn’t a disaster—it’s a puzzle, and the steps are straightforward if you take them one at a time. As a supplier, my goal isn’t just to sell a machine and walk away; it’s to make sure you have the tools to keep it running smoothly, even when a jam or misalignment pops up. If you’ve tried all the steps here and still can’t get your machine back up, or if you’re investing in a new chenille yarn machine and want support from a team that knows these machines inside and out, we’re here to help. Reach out to our team to discuss your production needs, get personalized troubleshooting support, or learn more about our line of durable, low-maintenance chenille machines built for both small and large scale production.
References
Yarn Winding Machine Chenille Yarn Machine Operation and Maintenance Manual. Industrial Textile Machinery Association, 2022.
Troubleshooting Guide for Textile Spinning Equipment. International Textile Manufacturers Federation, 2021.
Best Practices for Chenille Fiber Preparation and Processing. Journal of Textile Science and Engineering, vol. 8, no. 3, 2020, pp. 112-119.
Zhangjiagang Kingkangda Machinery Co., Ltd.
Zhangjiagang Kingkangda Machinery Co., Ltd. is one of the most professional chenille yarn machine manufacturers and suppliers in China, specialized in providing high quality customized service. We warmly welcome you to wholesale chenille yarn machine in stock here from our factory. Contact us for pricelist and quotation.
Address: Korea Industrial Park, Fenghuang Town, Zhangjiagang City, Jiangsu Province, China
E-mail: kingkangdacn@hotmail.com
WebSite: https://www.kingkangda.com/
